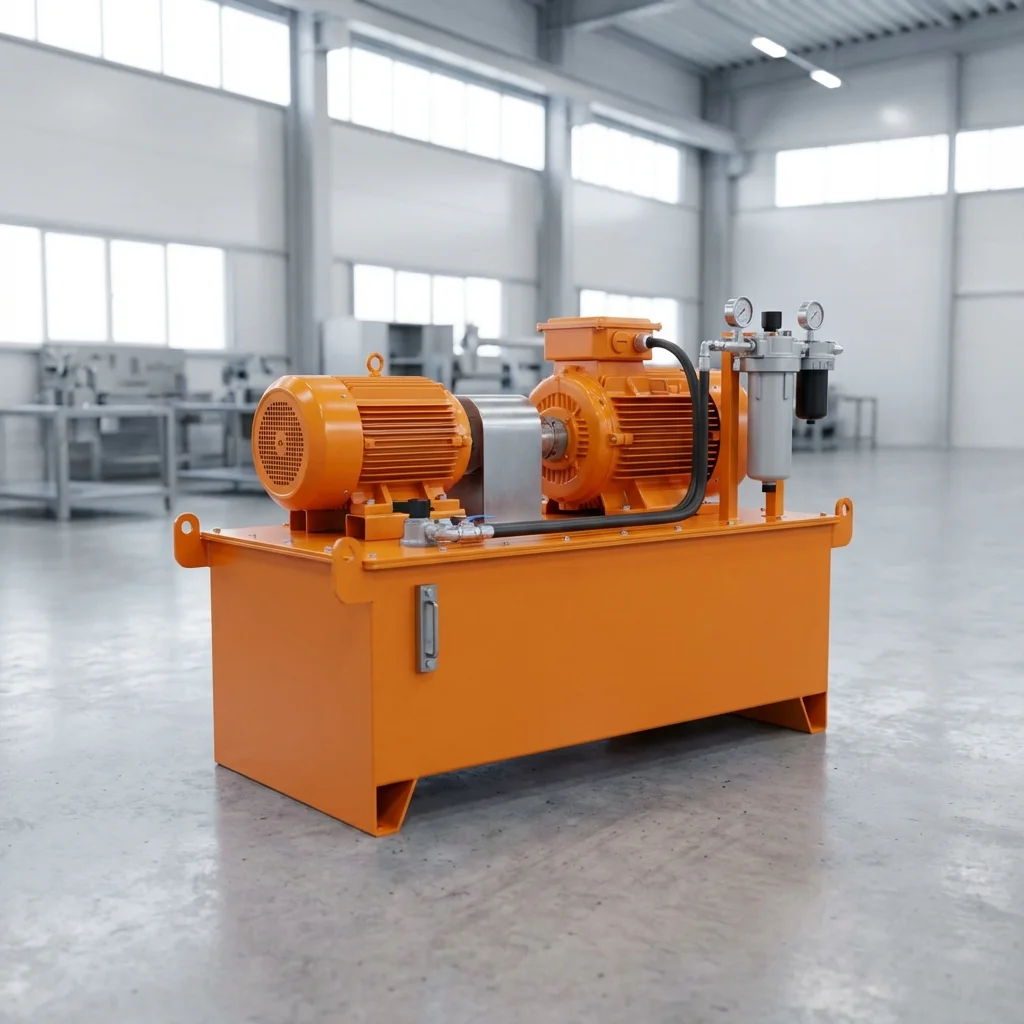
Rising energy costs have made hydraulic system efficiency a necessity rather than a
choice.
A
correctly optimized hydraulic system not only reduces energy bills but
also
extends component life, reduces breakdowns, and minimizes your carbon footprint.
Striking Statistic
Approximately 15-20% of total energy consumption in
industrial facilities originates from hydraulic and pneumatic systems.
Efficiency-focused modernization can achieve up to 30% savings in
this
consumption.
1. Key Factors Reducing Efficiency
There can be many reasons for a system running inefficiently. Energy loss usually turns
into
heat, creating "double damage" by increasing the system's cooling load.
1.1. Over-sizing
Electric motors and pumps selected larger than necessary with a "just in case" logic
always
operate below their optimum efficiency point. This unnecessarily increases both initial
investment costs and operating expenses.
| Source of Inefficiency
|
Problem Caused |
Suggested Solution |
| Internal
Leaks
|
Volumetric
efficiency loss, heating |
Seal/gasket
replacement, worn valve repair |
| Incorrect
Pipe
Diameter |
High pressure
drop (ΔP) |
Large
diameter
piping suitable for flow rate |
| Dirty
Filters |
Pump
cavitation, flow resistance |
Regular
filter replacement and monitoring |
| Incorrect Oil Selection |
Friction losses or leakage |
Viscosity selection suitable for operating
temperature
|
2. Transformation with Modern Technologies
Transitioning from traditional fixed displacement systems to modern technologies can
surprisingly shorten the return on investment (ROI).
2.1. Load Sensing Systems
Load sensing pumps generate only the flow and pressure required by the system. In
standby
situations where there is no load, energy consumption drops to almost zero.
2.2. Variable Frequency Drives (VFD)
Inverter systems that adjust the speed of the electric motor according to hydraulic
demand
are the pinnacle of energy saving. Motor speed rotating in vain at constant speed is
becoming
history.
"Efficiency is not a one-time setting, but a continuous process. Even the most
modern
system will lose efficiency over time without periodic analysis."
— BRS PROSES Engineering Team
3. Heat Management: The Hidden Energy Thief
Heat = Lost Energy
If your hydraulic system operates above 60°C,
something
is wrong. Excessive heat is the most concrete proof of lost energy spent in the
system
but not converted into work.
Heating problems usually stem from either insufficient cooling capacity or (more
frequently)
unnecessary pressure losses in the system. As BRS PROSES, we detect
"hot
spots" in your system with thermal camera analysis and eliminate the source of
inefficiency.
4. Energy Audit with BRS PROSES
We offer a professional roadmap to increase your business's energy efficiency:
- Flow, pressure, and power
analysis
of the existing system
- Leak
detection via thermal imaging
- Revision cost and return on
investment (ROI) calculation
- On-site modernization and
commissioning
- Personnel training
Suction Line Hydraulics & Net Positive Suction Head (NPSH)
Cavitation in hydraulic pumps is overwhelmingly caused by flawed suction line design. To guarantee adequate inlet filling, the fluid absolute pressure at the pump inlet port must remain comfortably above the fluid vapor pressure under all operating temperatures.
BRS PROSES engineering rules require suction line fluid velocities to remain between 0.5 m/s and 1.0 m/s (calculated as $v = �rac{Q}{6 cdot pi cdot d^2}$). Suction line vacuum must never exceed -0.2 bar (-150 mmHg) gauge pressure. Emitters must incorporate full-flow ball valves with limit switches preventing pump motor startup when the suction isolation valve is closed.
Pump Performance Metrics: Volumetric vs Hydromechanical Efficiency & Noise Abatement
Specifying an industrial hydraulic pump involves balancing mechanical efficiency, pressure ceiling, acoustic noise emissions, and fluid contamination tolerance. Overall pump efficiency ((η_{total})) is the product of two distinct internal behaviors: Volumetric Efficiency ((η_v)) and Hydromechanical Efficiency ((η_{hm})):
η_total = η_volumetric × η_hydromechanical
• Volumetric Efficiency: Decreases at higher pressures due to internal slippage across clearances (piston slippers, gear side plates).
• Hydromechanical Efficiency: Decreases at lower speeds or high fluid viscosities due to shearing friction between moving metallic surfaces.
| Pump Architecture |
Pressure Limits |
Typical Overall Efficiency |
Noise Level dB(A) |
| External Gear Pump |
Up to 250 bar |
75% – 85% |
72 – 82 dB(A) |
| Variable Vane Pump |
Up to 160 bar |
80% – 88% |
62 – 68 dB(A) (Quiet) |
| Axial Piston (Swashplate) |
Up to 420 bar |
90% – 95% |
74 – 80 dB(A) |
Technical Field Inspection & Commissioning Protocol
Prior to signing off on any fluid power retrofit, system upgrade, or routine component overhaul, technical commissioning engineers must rigorously complete the following verification procedures to ensure full compliance with ISO machinery safety standards:
- Static Hydrostatic / Pneumatic Pressure Proof Test: Pressurize circuit to 1.5× maximum design working pressure for 15 minutes, inspecting all welded flanges and fittings for micro-weeping.
- Contamination & Fluid Particle Verification: Draw dynamic fluid samples under working temperature and confirm ISO 4406 cleanliness classes (or ISO 8573-1 air dew point classes) before activating sensitive proportional spool valves.
- Thermal Baseline Profiling: Record continuous thermal infrared scans of pump casings, valve manifold manifolds, and accumulator bodies across 4 hours of full-load production cycles to confirm proper thermal dissipation.
- Failsafe & Emergency De-energization: Verify manual LOTO isolation valves, dump valves, and accumulator vent blocks discharge trapped hydraulic/pneumatic kinetic energy to 0 bar within 2.0 seconds of emergency e-stop triggering.